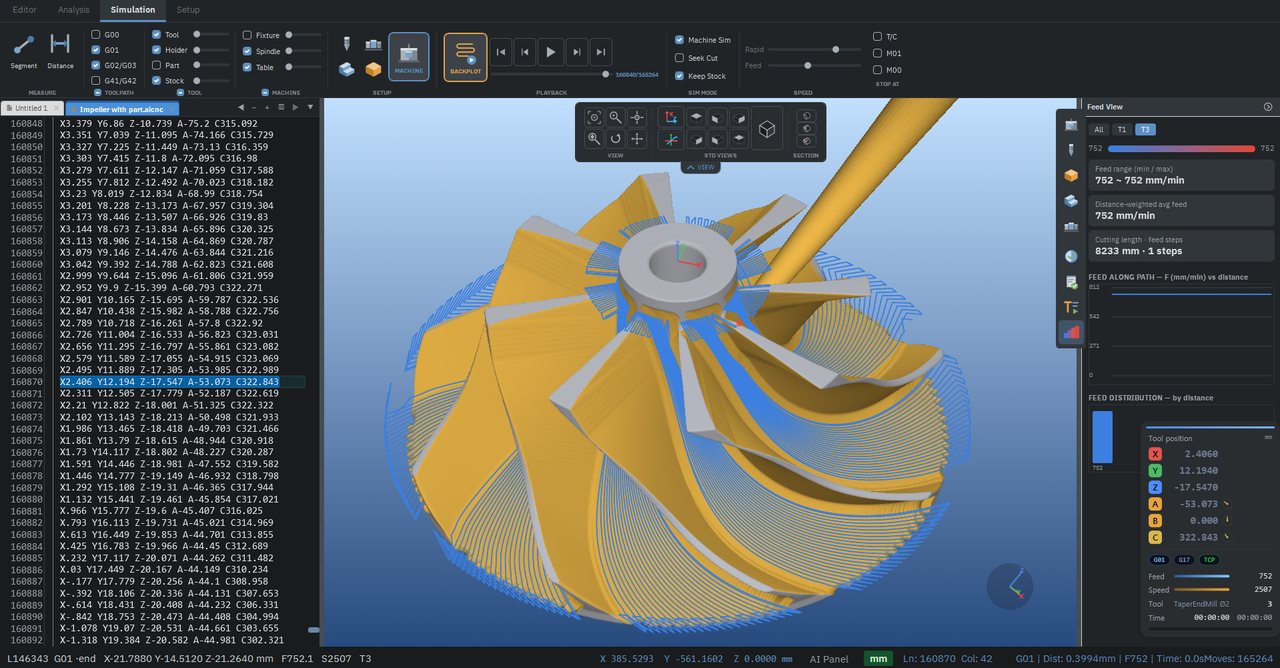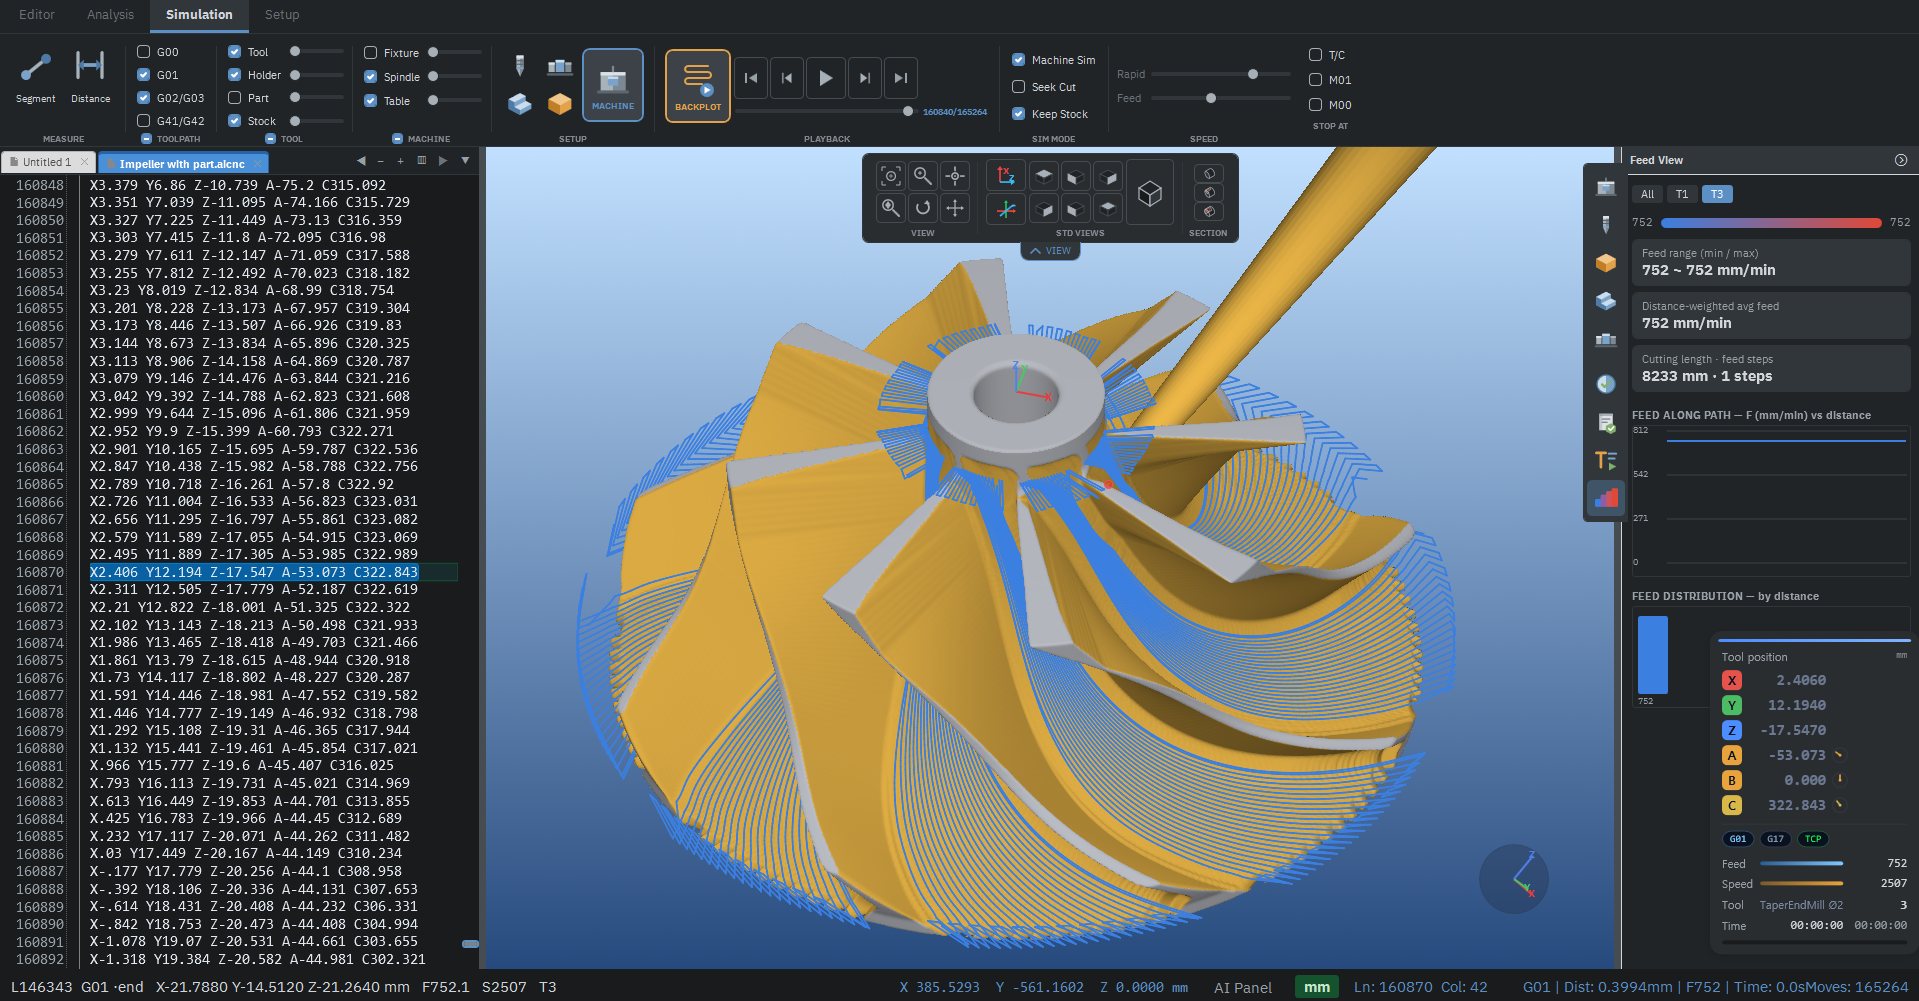
AicncX on screen — simultaneous 5-axis impeller toolpath and cut simulation
NC verification & 3D machining simulation

Before the machine cuts,
the program is verified on screen.

AicncX reads your machine's real kinematics and each controller's own G-code, and reproduces the cut as it happens. Over-cuts, multi-channel sync and macro call maps are all verified before the job starts.

5-axis simultaneousB-axis mill-turnSwiss 2 channelsTurn-mill 2 turretsWire EDM
Inside AicncX

What you actually see

The code on one side, the verified path on the other. These are real screens.
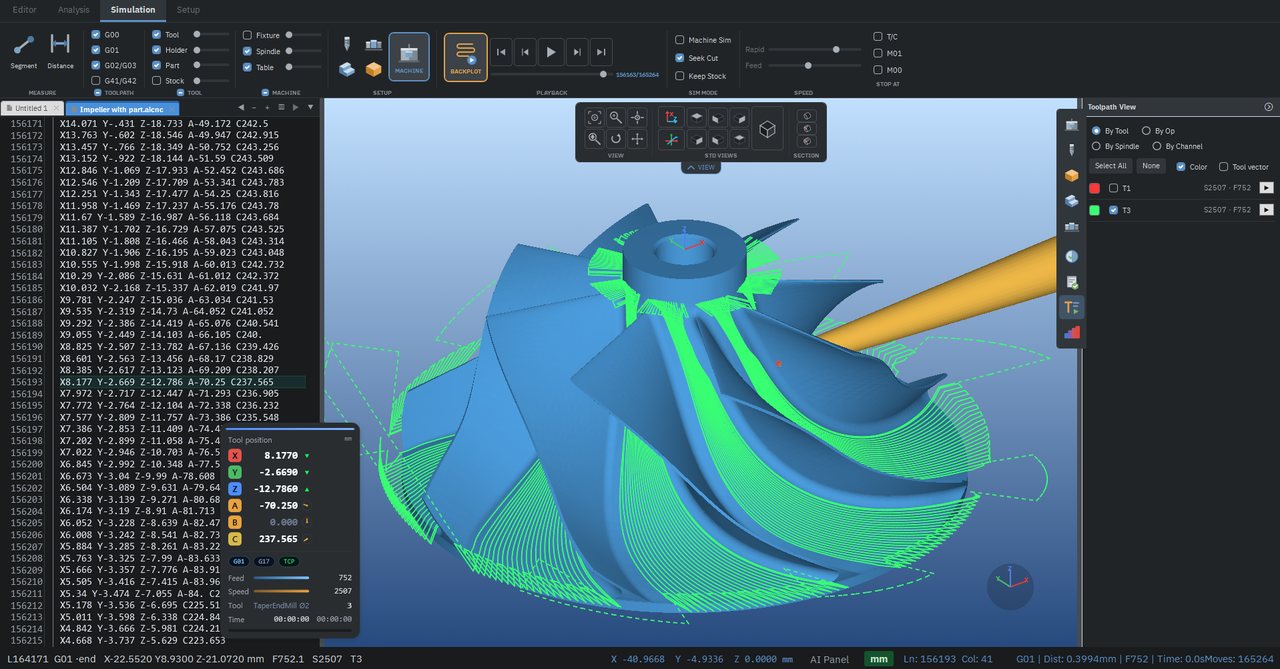
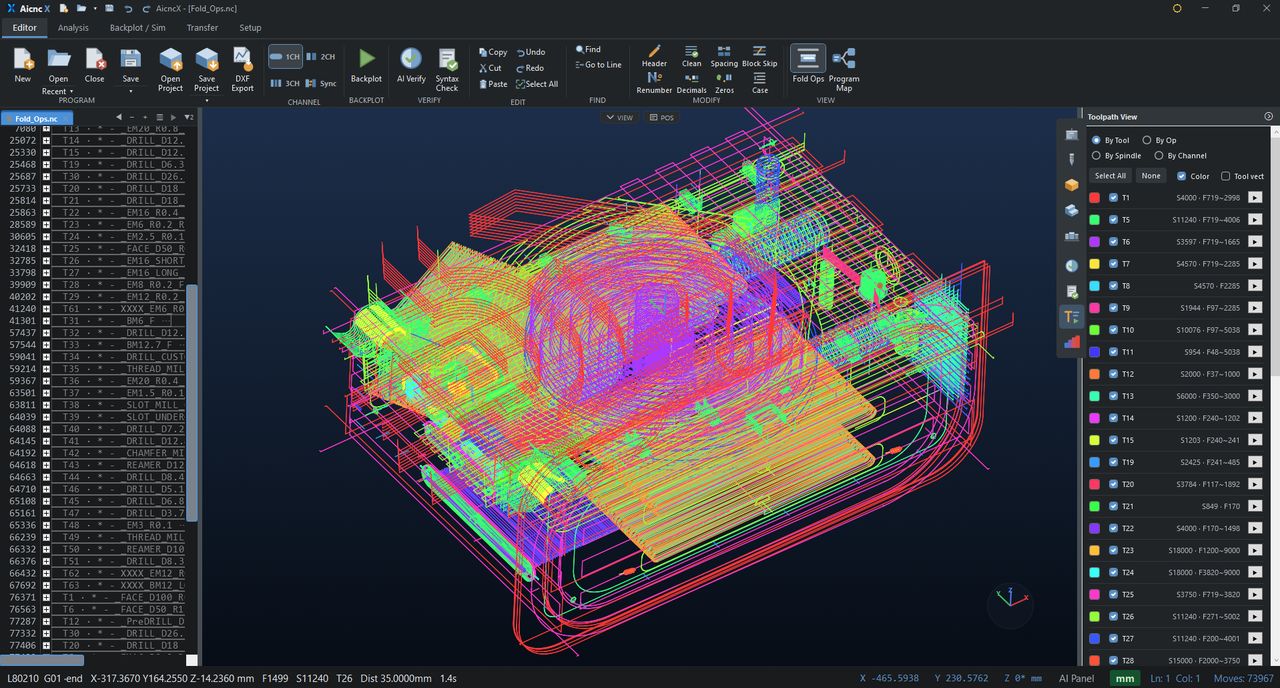
Toolpath view
Toolpath viewFilter by tool, operation, spindle or channel and keep only the paths you want. Colour each one and show the tool-axis vector.
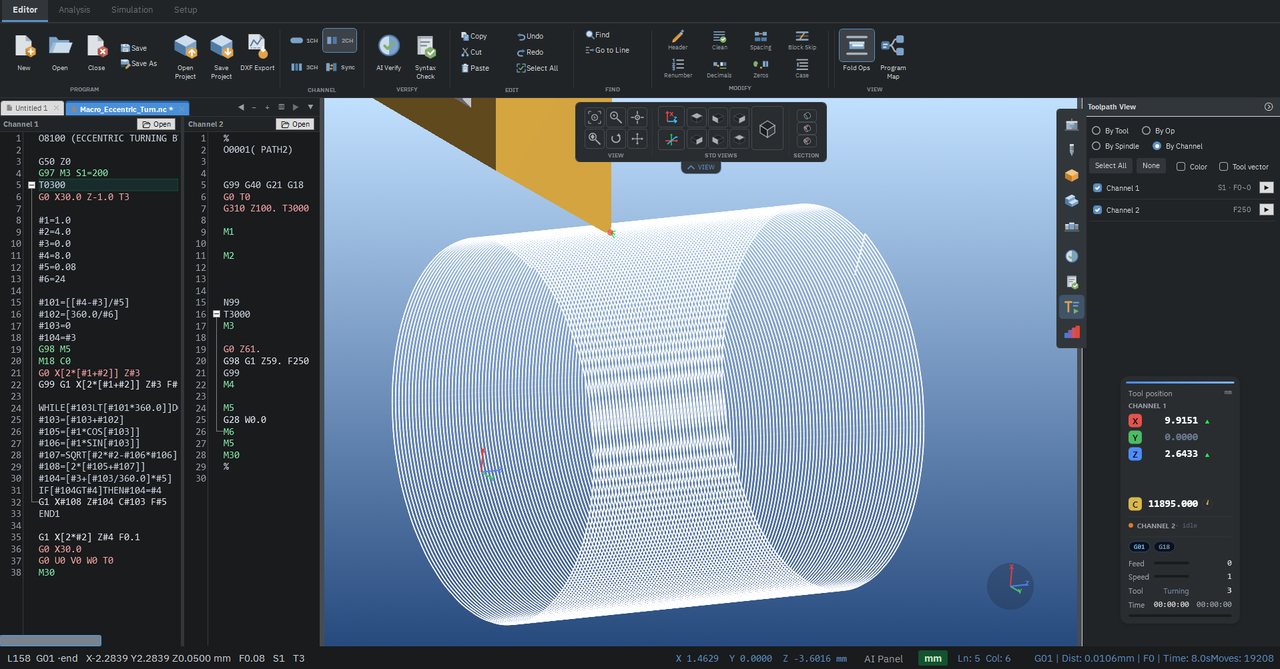
Two channels & macros
Two channels & macrosEdit channel 1 and 2 side by side and check their sync waits. WHILE, IF and variables are actually evaluated, so a macro program draws a real path.
Fold by operation
Fold by operationFold a program of tens of thousands of lines by tool or operation. Each operation has its own colour, so you see at a glance which code cuts where.
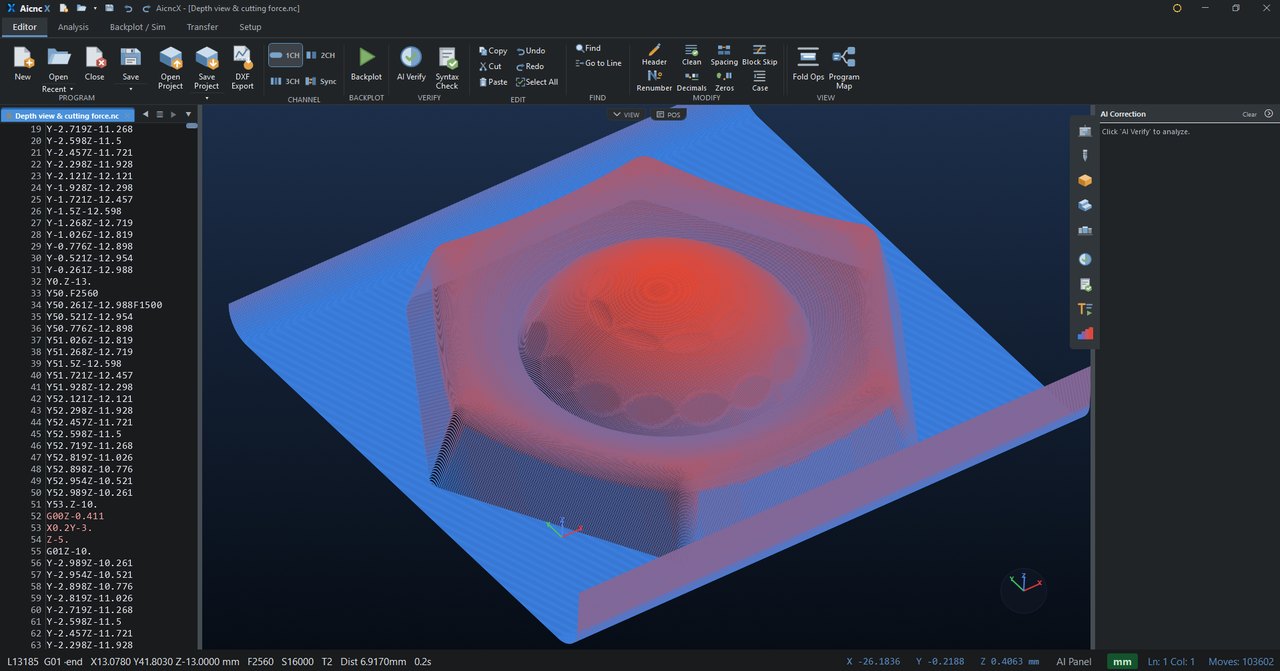
Depth view & cutting force
Depth view & cutting forceZ depth is colour-mapped so gouges and leftover stock stand out. Enter the material and tool and it computes cutting force and required power.
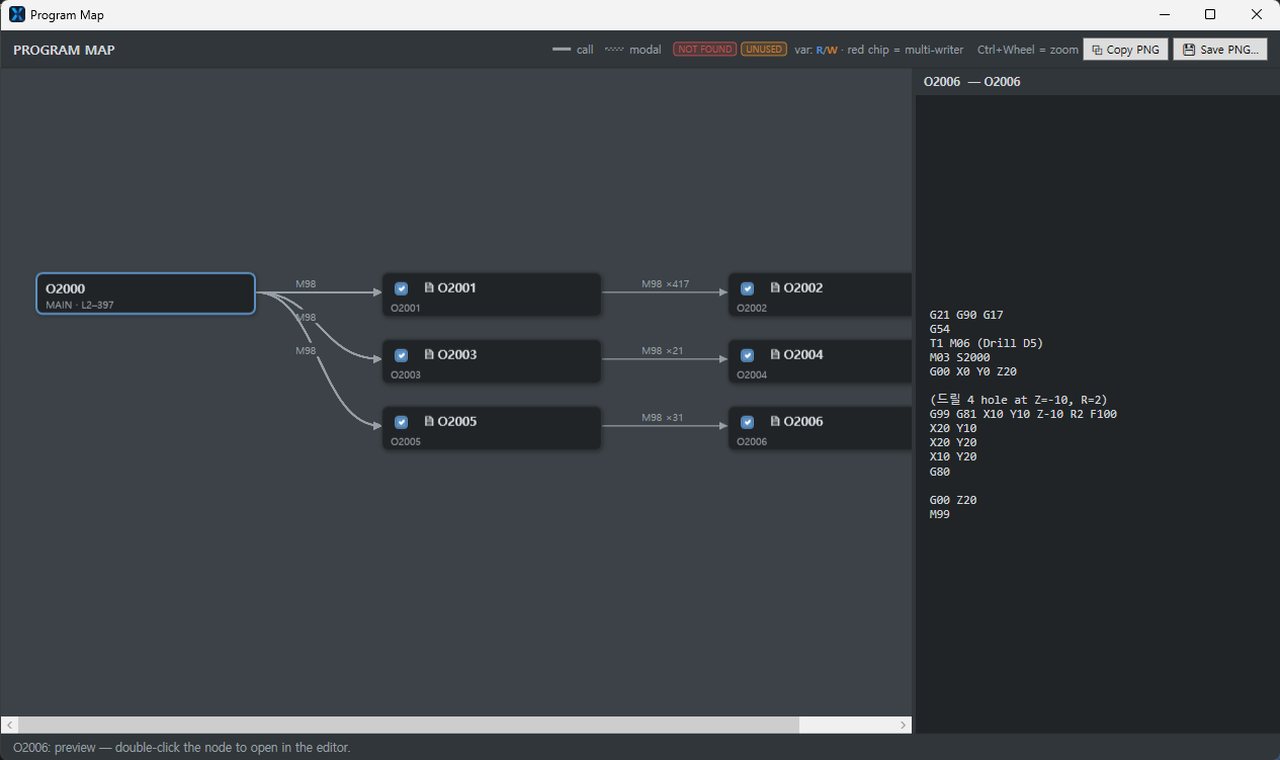
Program map
Program mapSee how main and subprograms call each other, with call counts, missing numbers and never-used programs flagged.
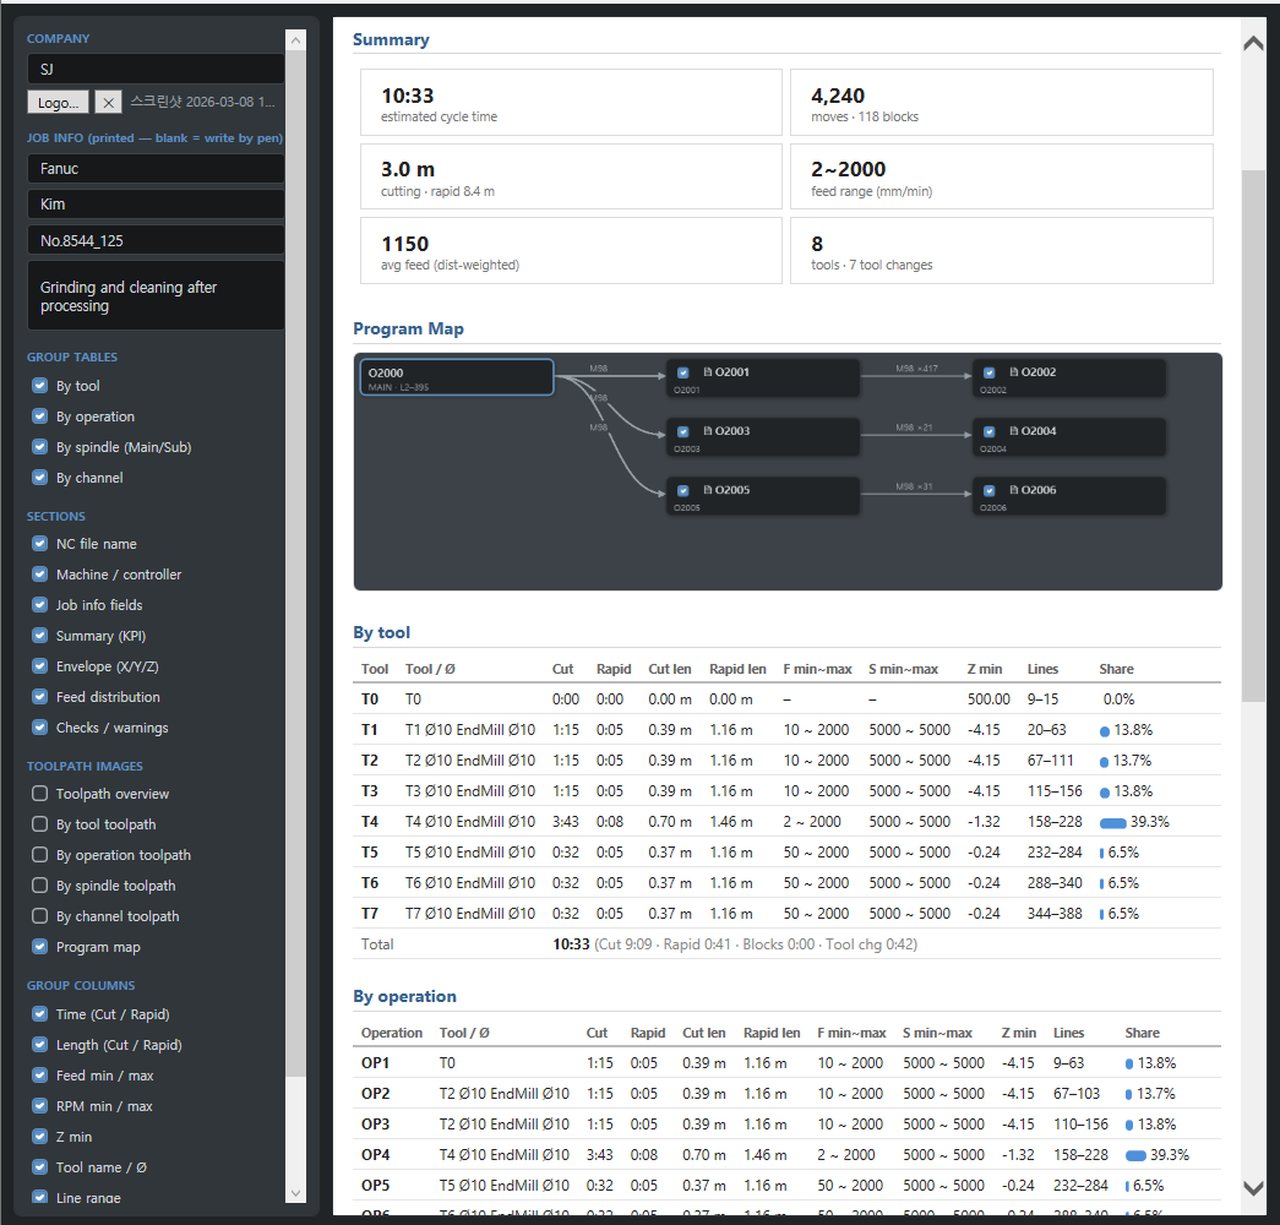
Job report
Job reportCycle time, cut length and feed range per tool, and the program map on a single sheet. Print it or export a PDF for the shop floor.
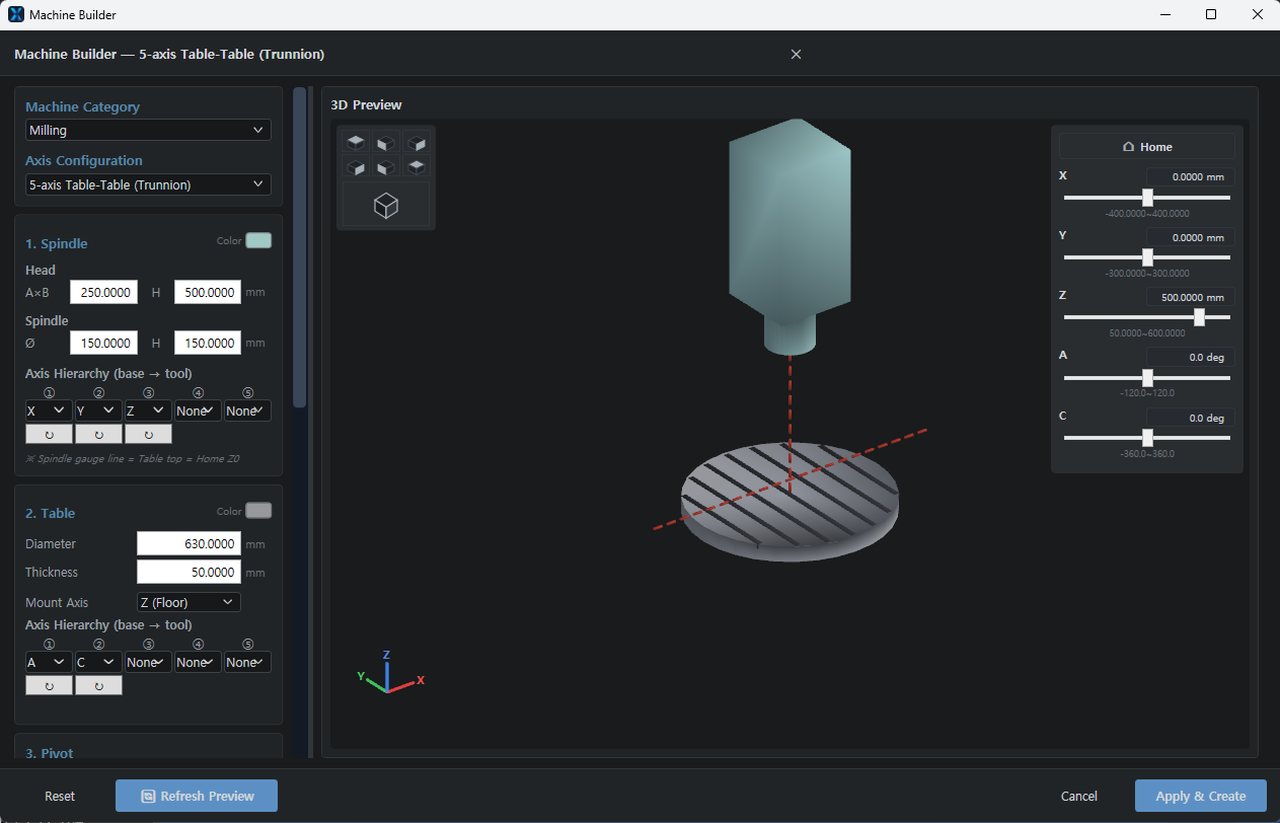
Machine builder & controls
Machine builder & controlsFanuc, Siemens, Heidenhain, Okuma, Mazak, Haas and Mitsubishi controls, covering 3-, 4- and 5-axis milling, simultaneous 5-axis, two-channel turn-mill, B-axis mill-turn and Swiss lathes. Pick the machine class and axis layout, enter the head and table sizes, the axis hierarchy and the pivot, and it is built in 3D.
Voxel stock simulation & part compare
Voxel stock simulation & part compareA GPU voxel engine cuts the stock with the real insert contour. Machined faces are coloured per tool, so you see at once which tool left what. Compare the machined stock against the finished-part STL and it is painted by tolerance band, so over-cut and under-cut areas stand out in colour.
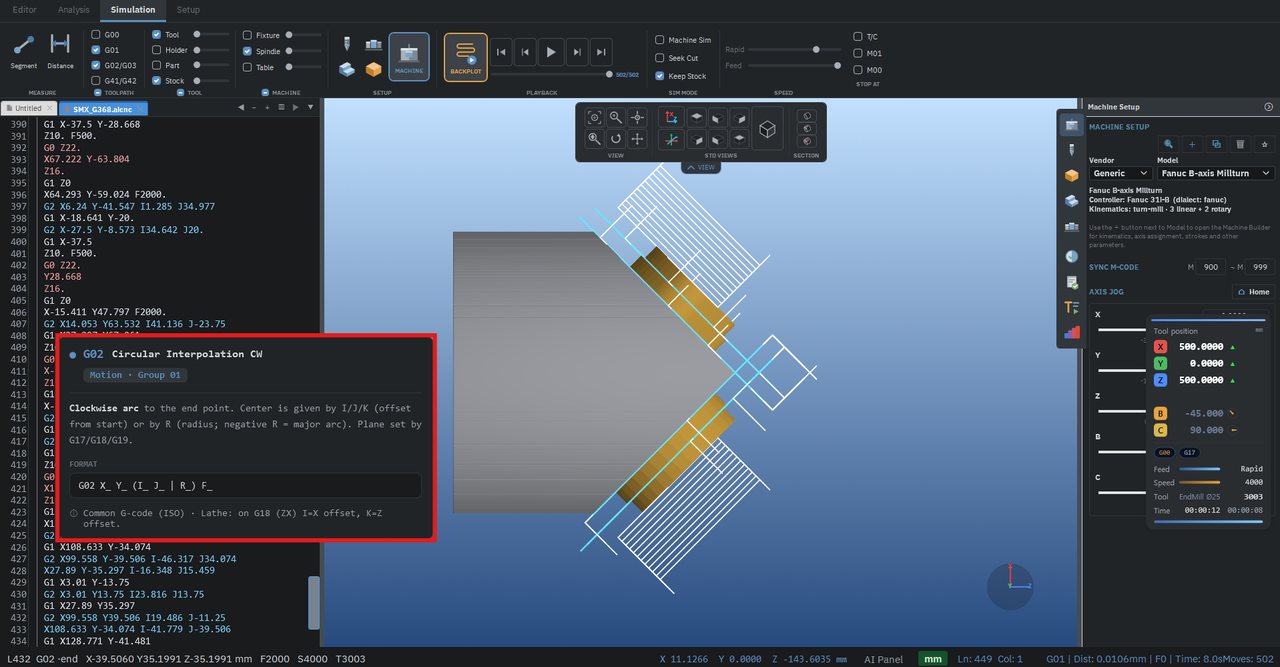
G/M code & macro help
G/M code & macro helpHover a code and a tooltip gives its meaning, its format and the catch to watch for. Macro variables are explained too, and the UI ships in 15 languages, so unfamiliar code reads straight away.
Wire EDM
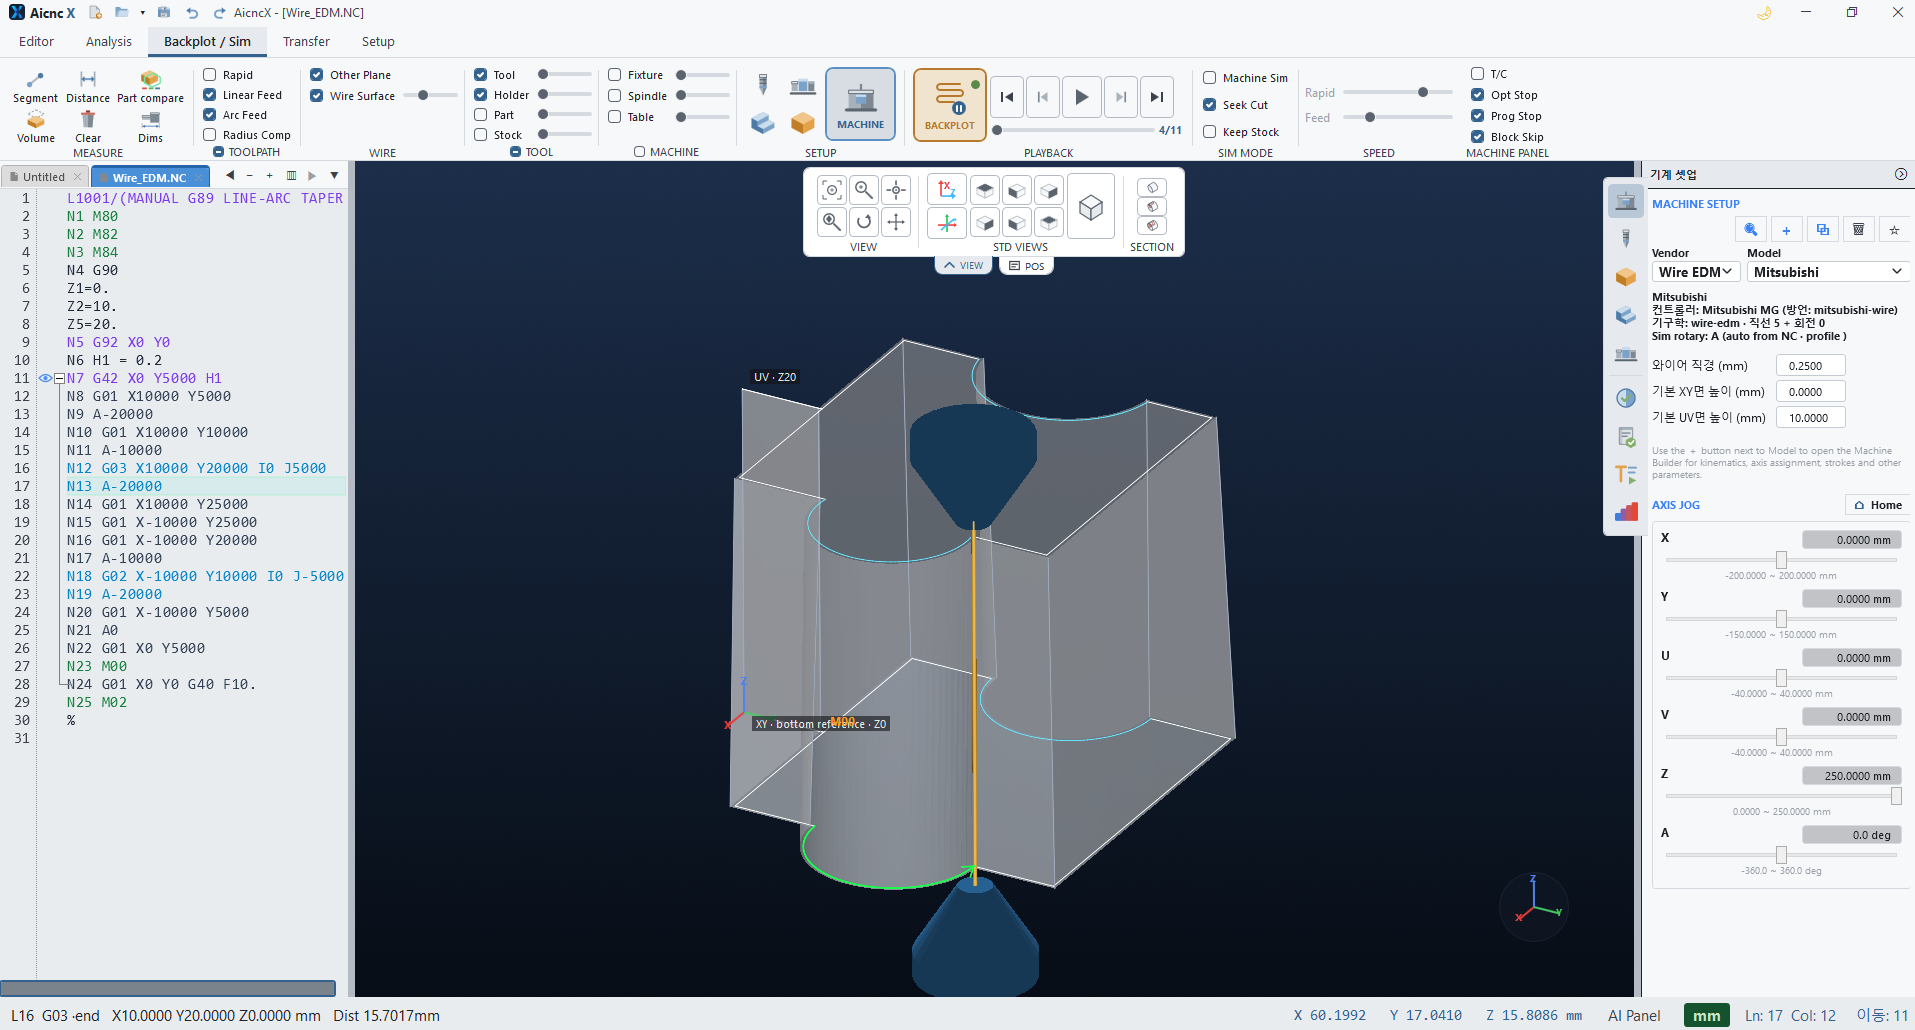
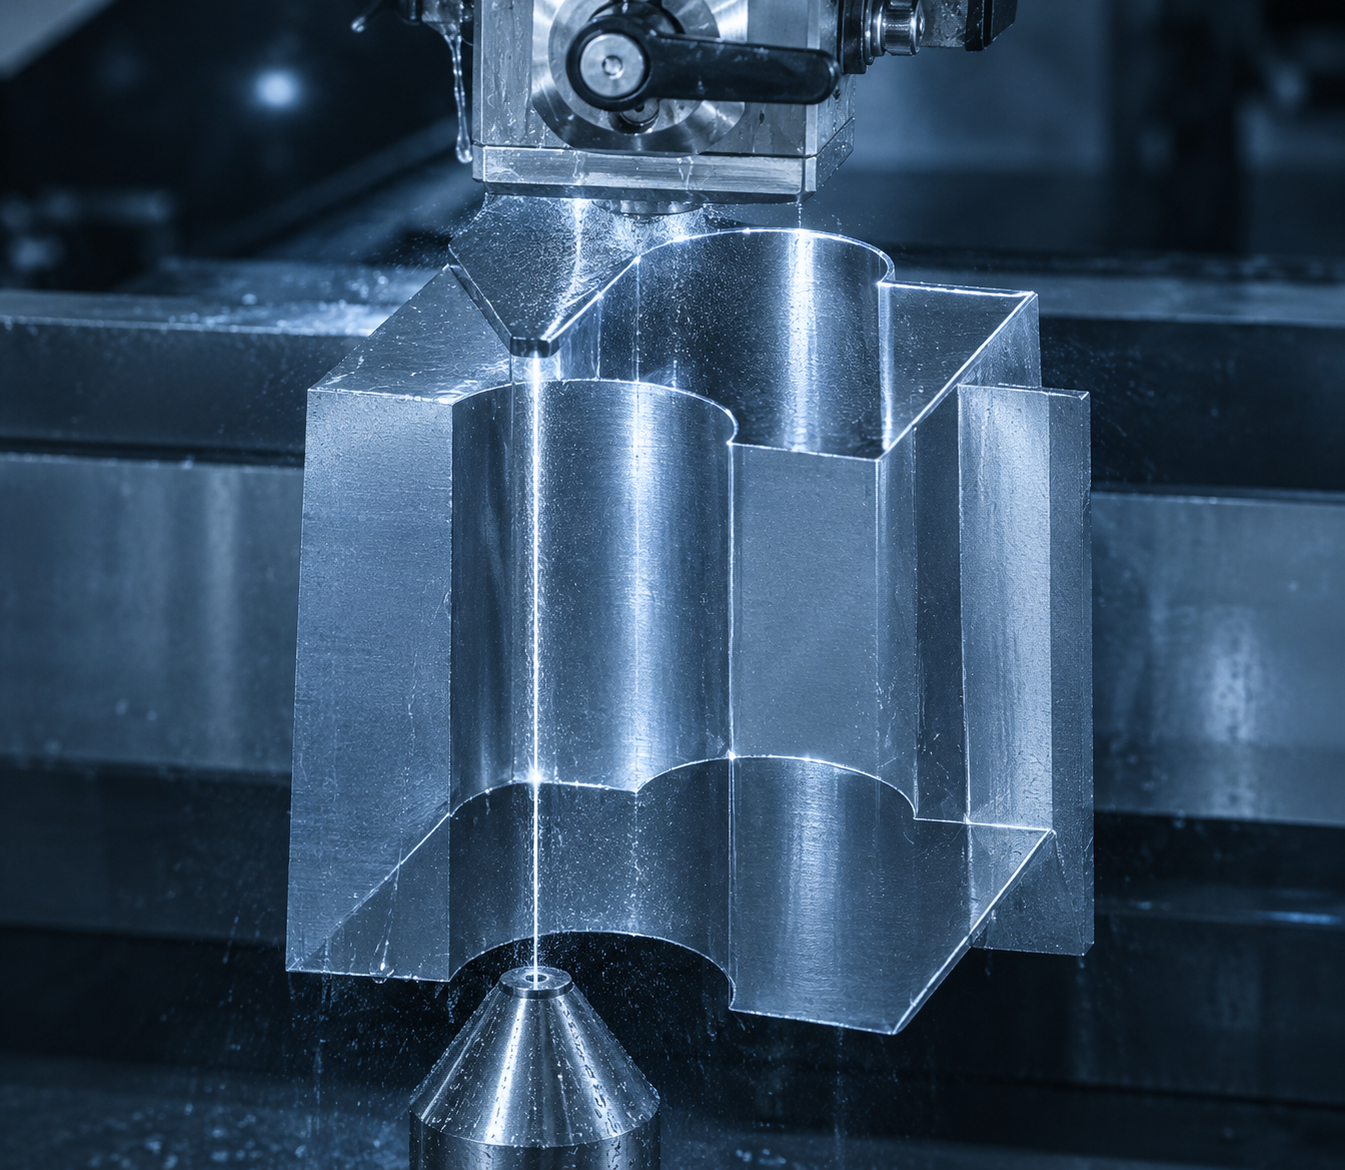
Wire EDMReads wire-EDM programs just as the control does and draws the upper and lower taper path. Per-pass offset, technology files, thread and cut points and punch/die direction are all shown.
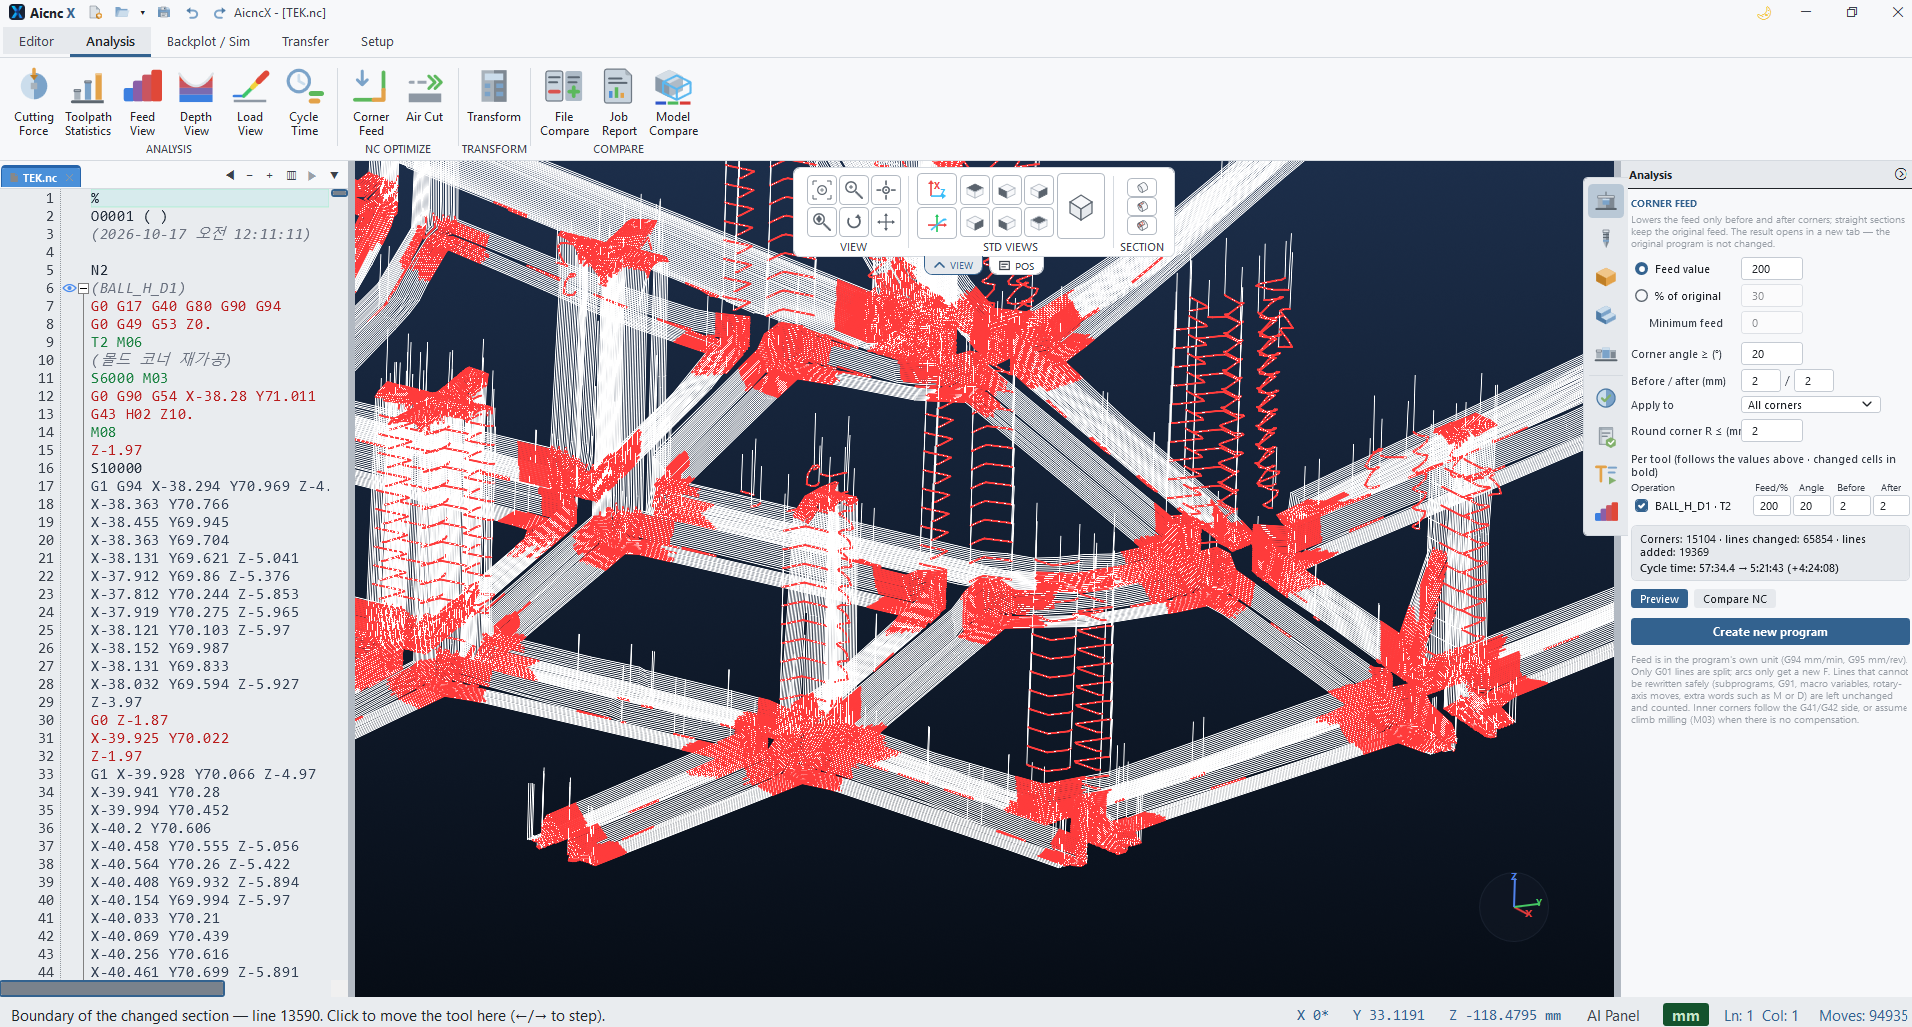
Corner feed
Corner feedGenerates a new program that lowers the feed only around corners, easing tool load and over-cut. Set the corner angle, round radius and lead-in/out distance, and a preview paints the slowed spans.
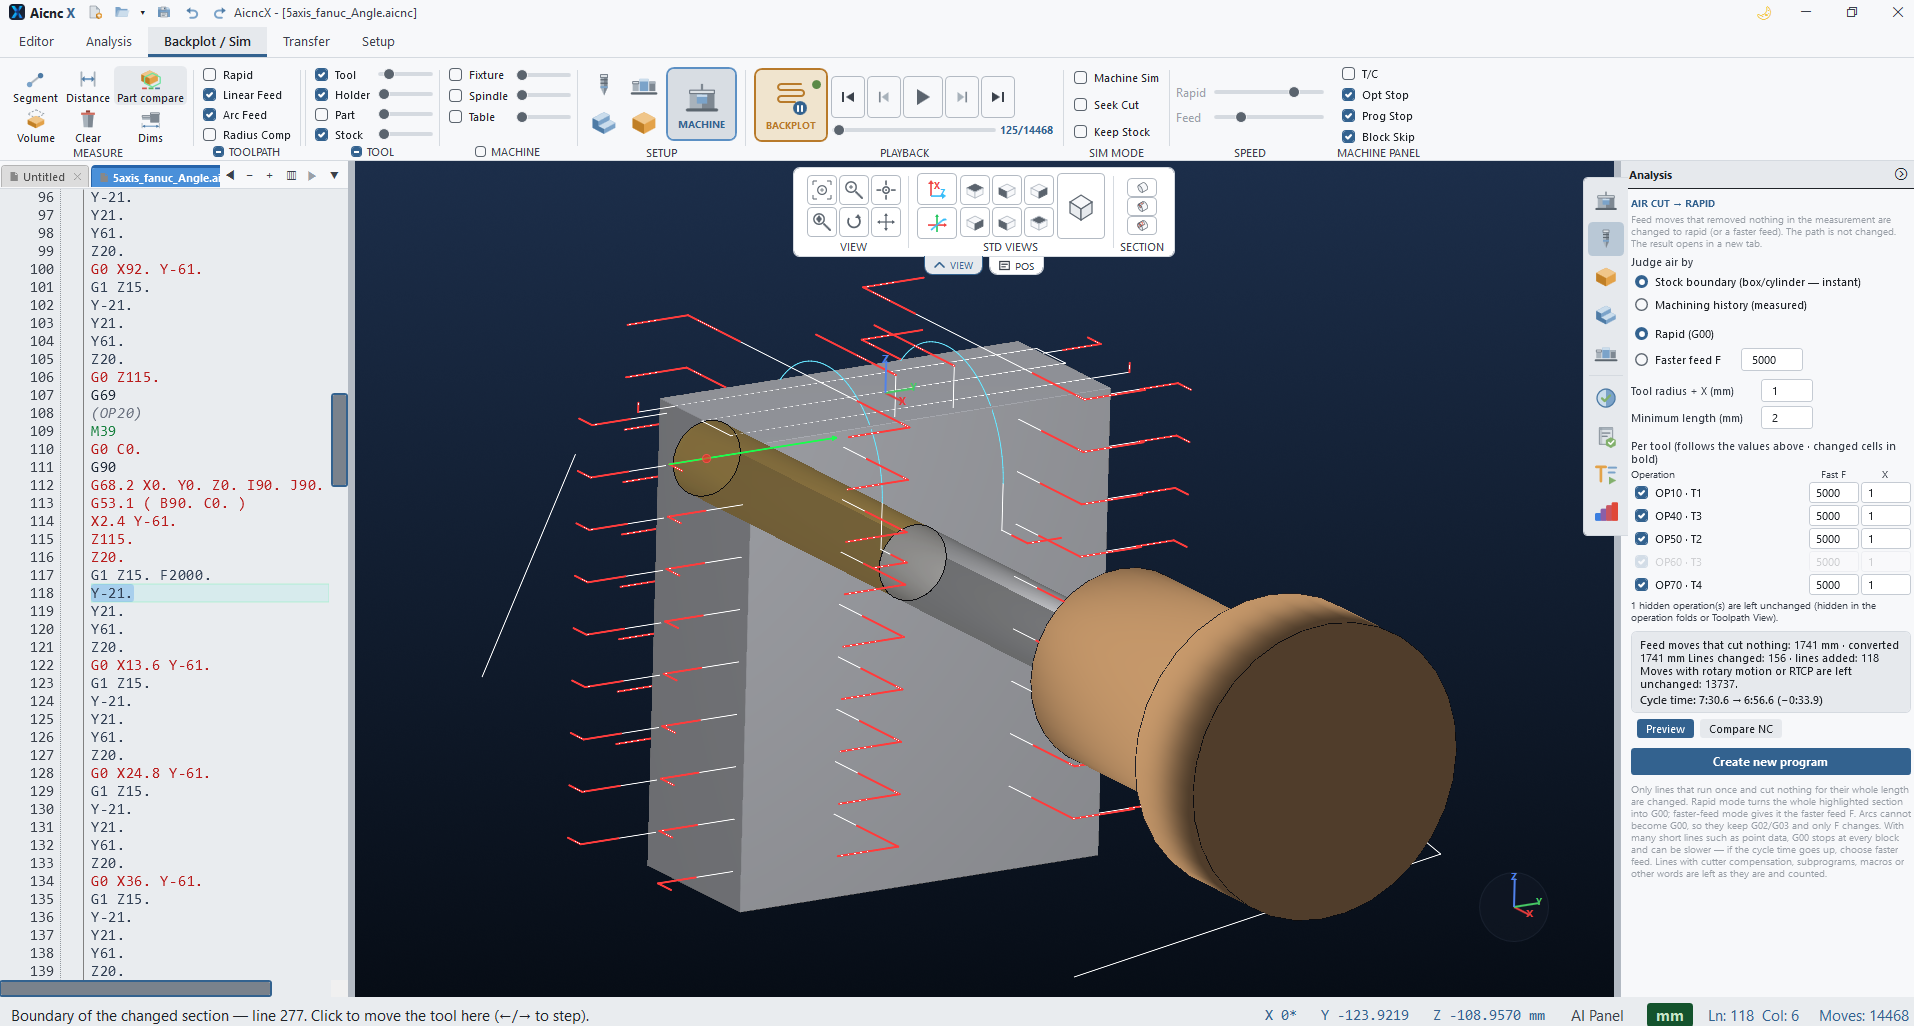
Air-cut trimming
Air-cut trimmingFinds feed moves that travel through air without cutting, judged from the stock boundary and the machining history. A preview marks air moves in red so you can turn them into rapids or trim them and cut cycle time.
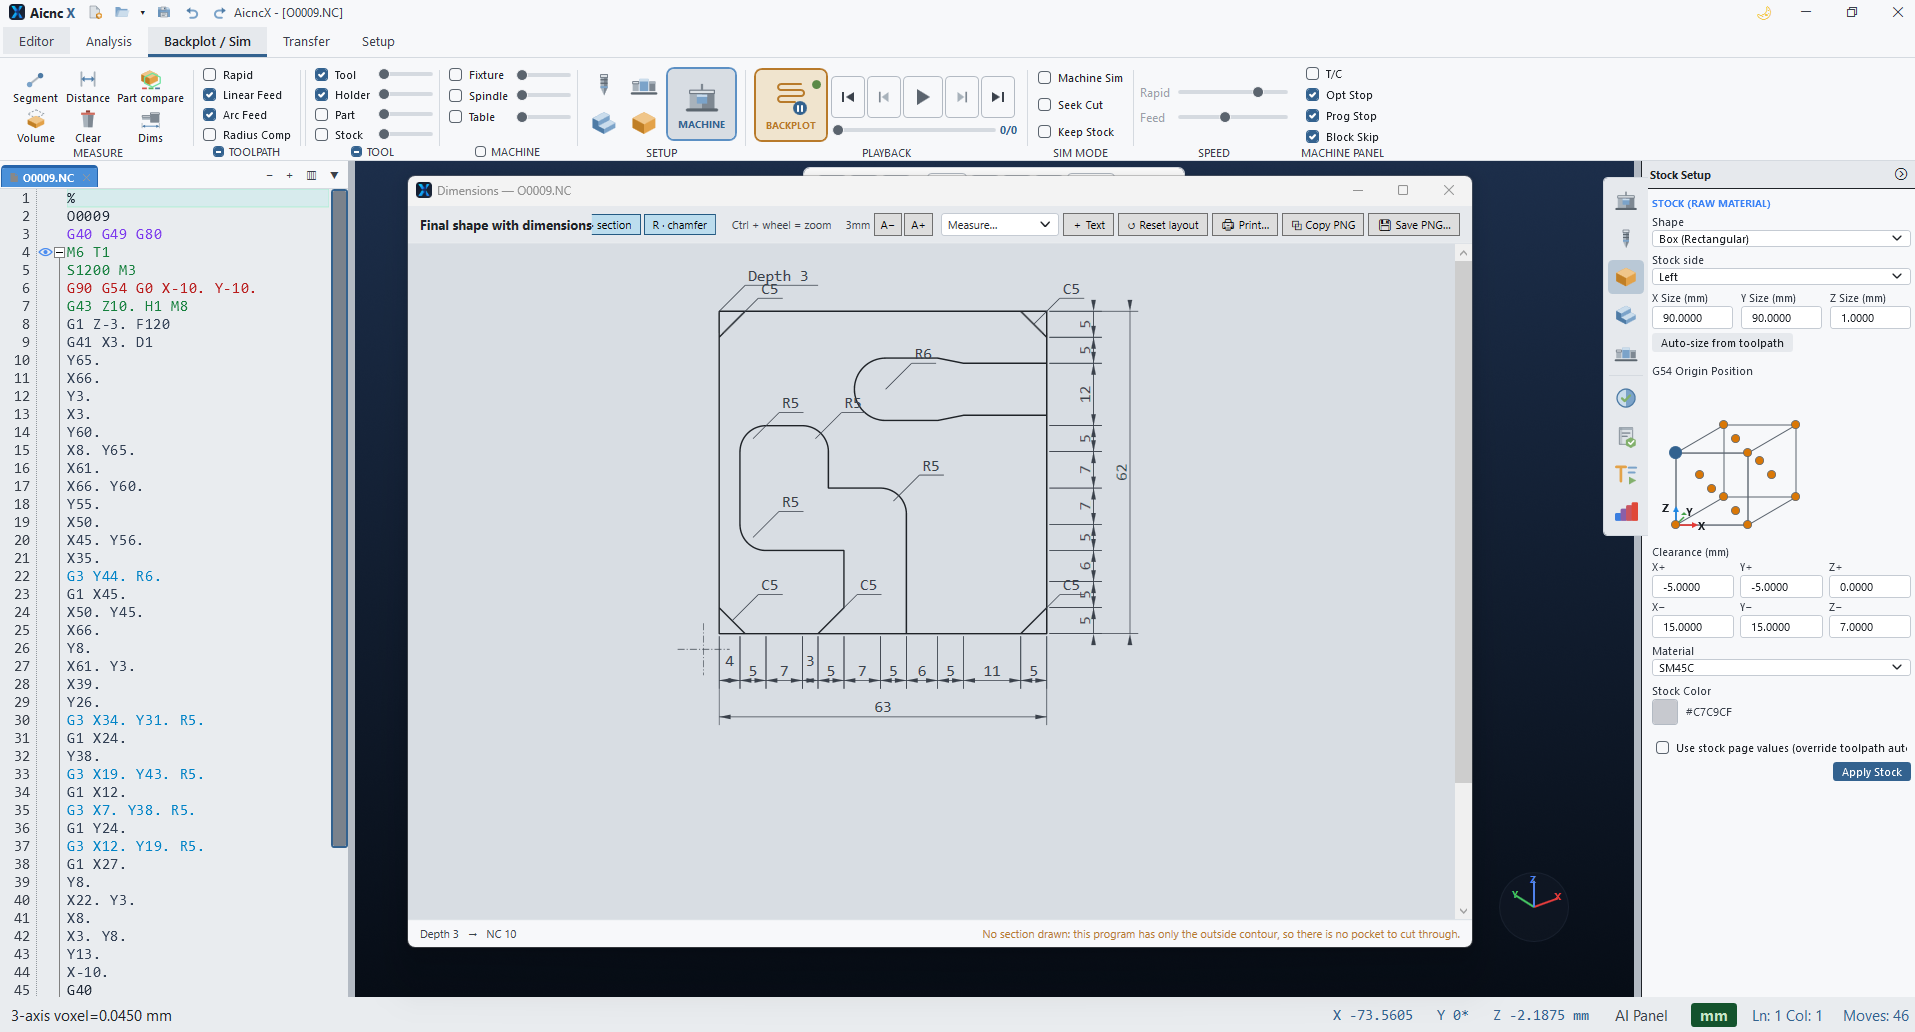
Academy — milling
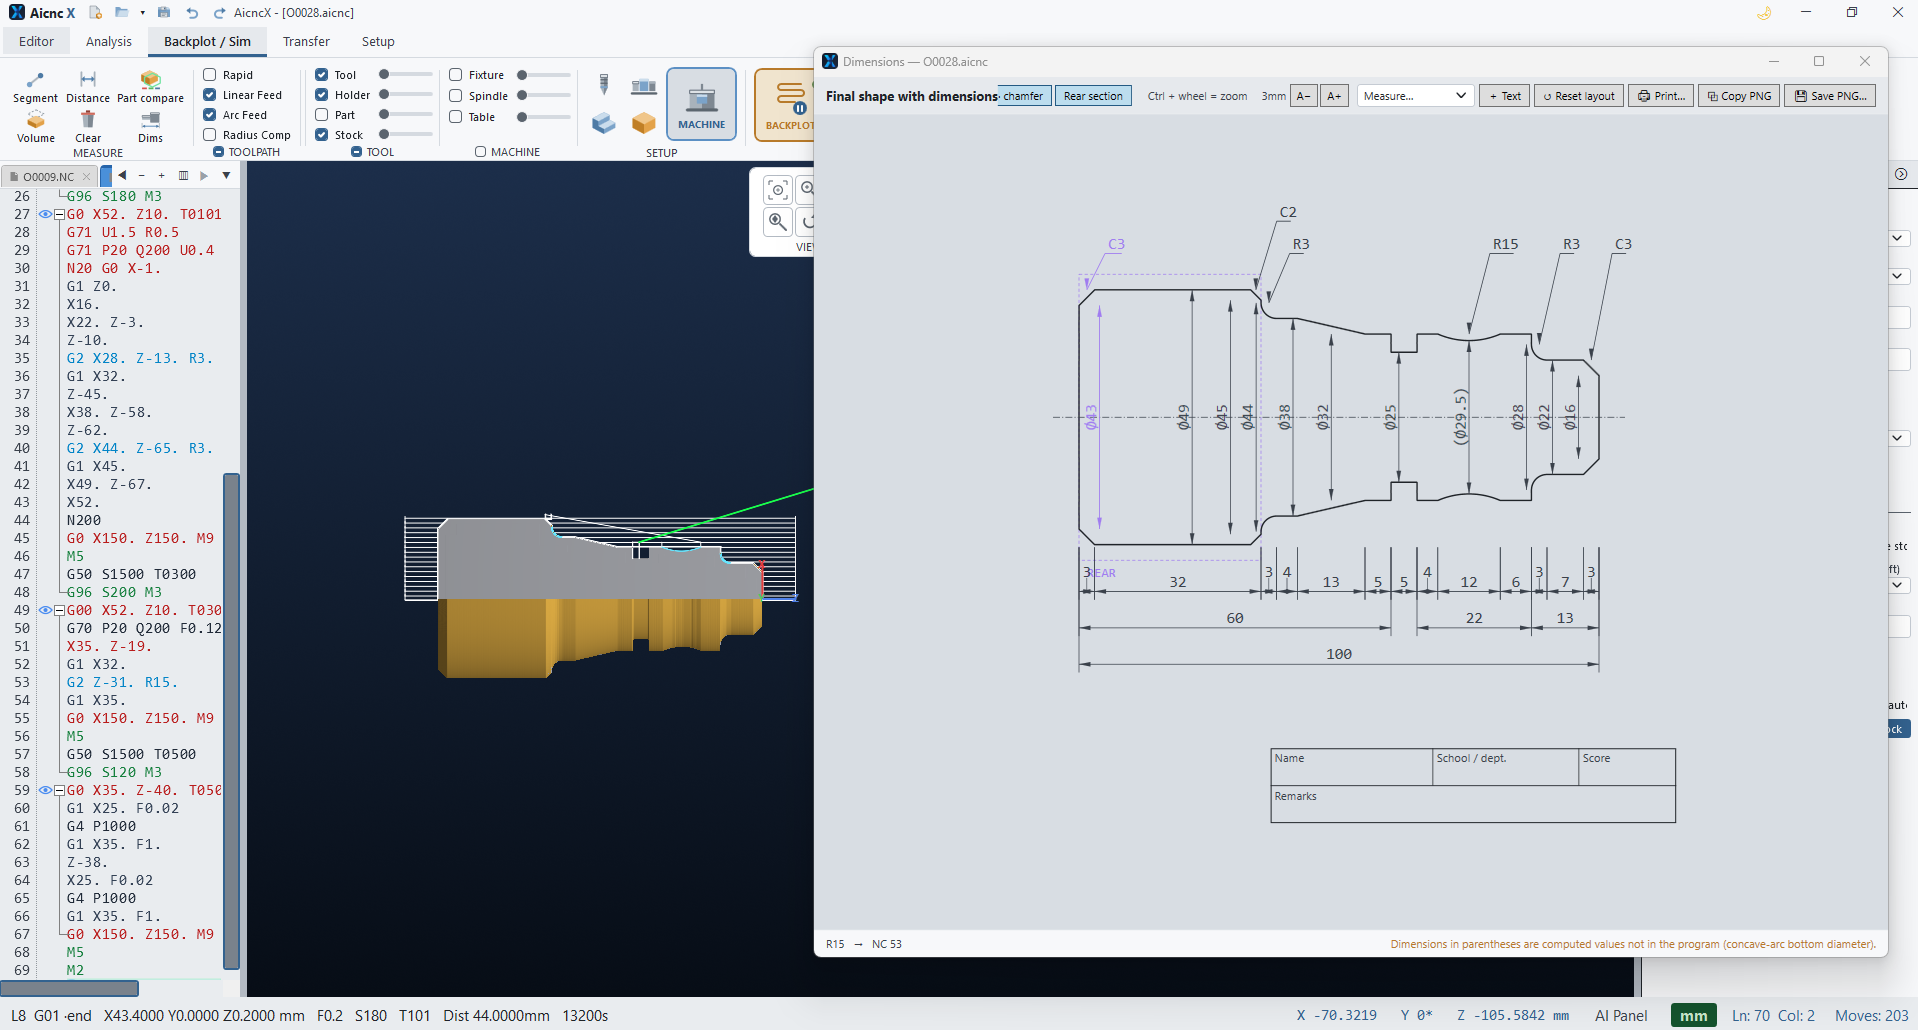
Academy — millingA mode for training and practical exams. It adds exam-style dimension sheets and 3D model compare against the finished part, checking a student's deviation by tolerance and reporting pass or fail.
Academy — lathe
Academy — latheFor lathe practicals, with diameter and length dimension sheets, back-working flip and finished-model compare. Over-cut and under-cut are colour-coded, ready for grading.
DNC transfer
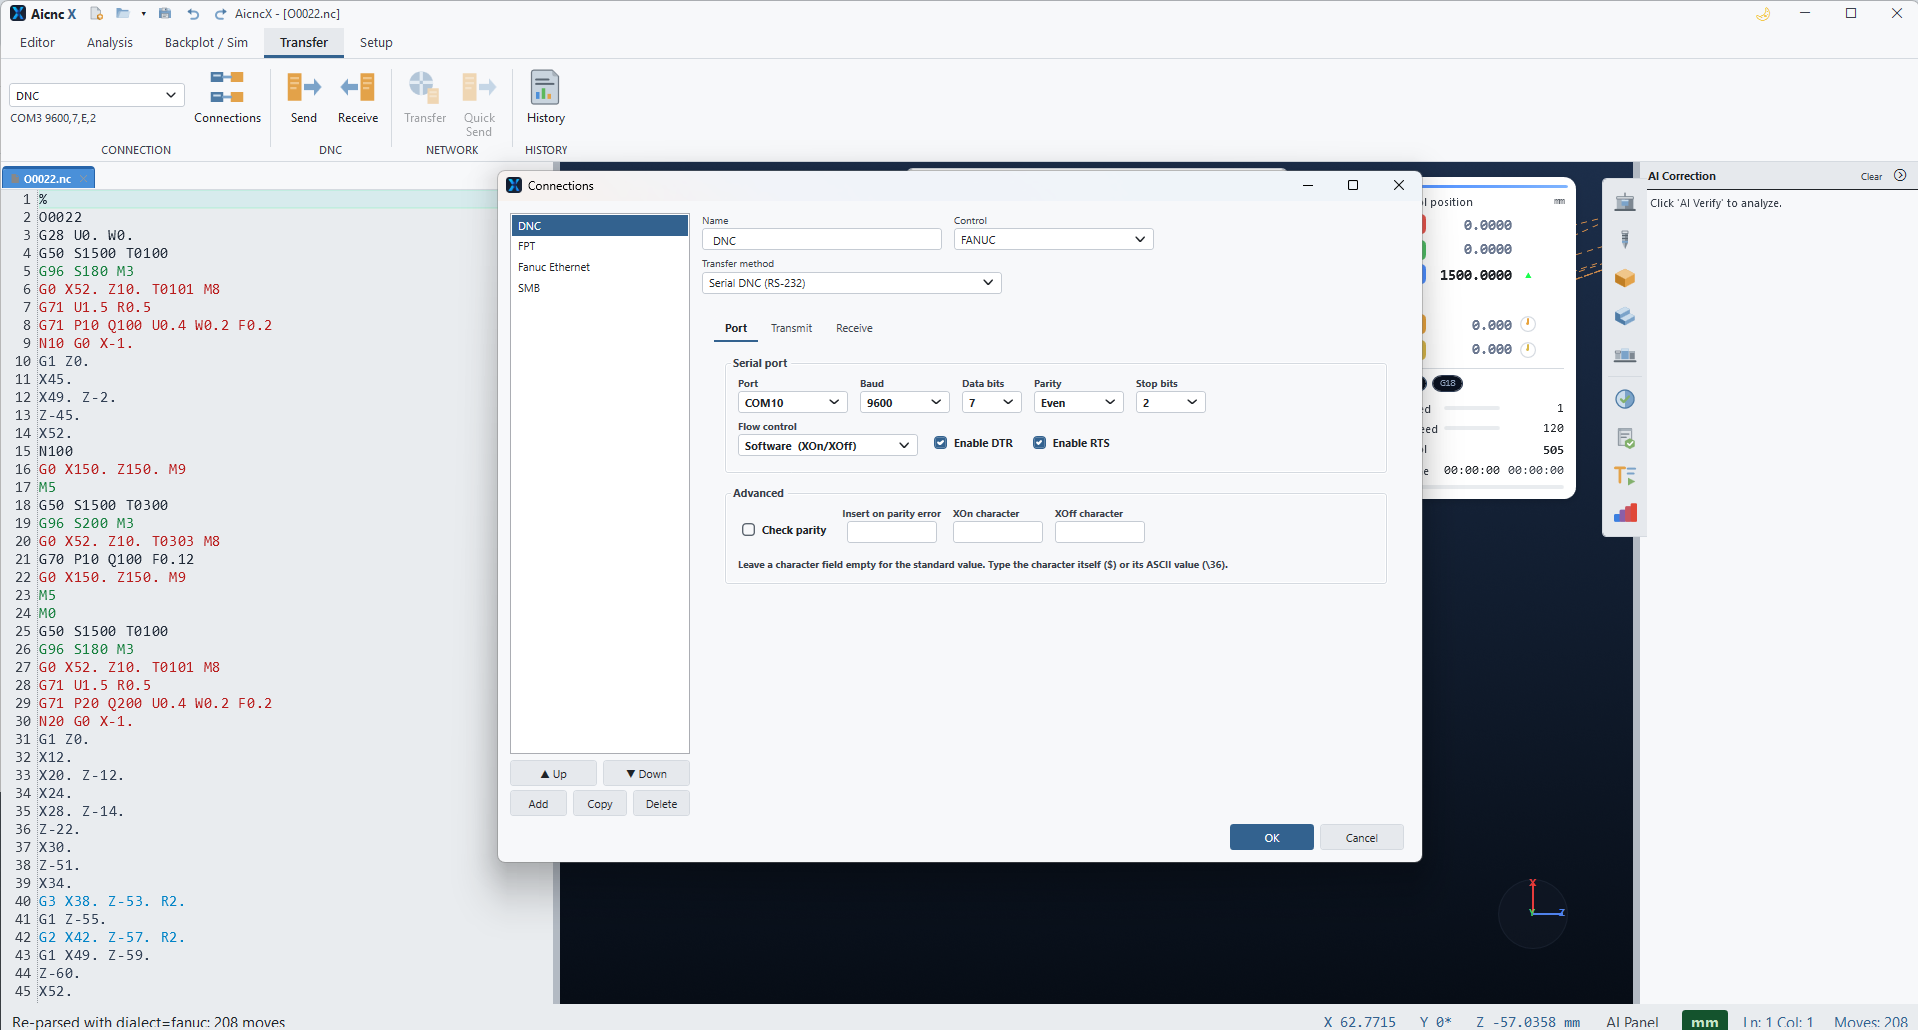
DNC transferSend verified NC programs straight to the machine and receive them back. Serial DNC (RS-232) plus FTP, Ethernet and shared-folder (SMB) transfer are supported, with saved connection profiles.
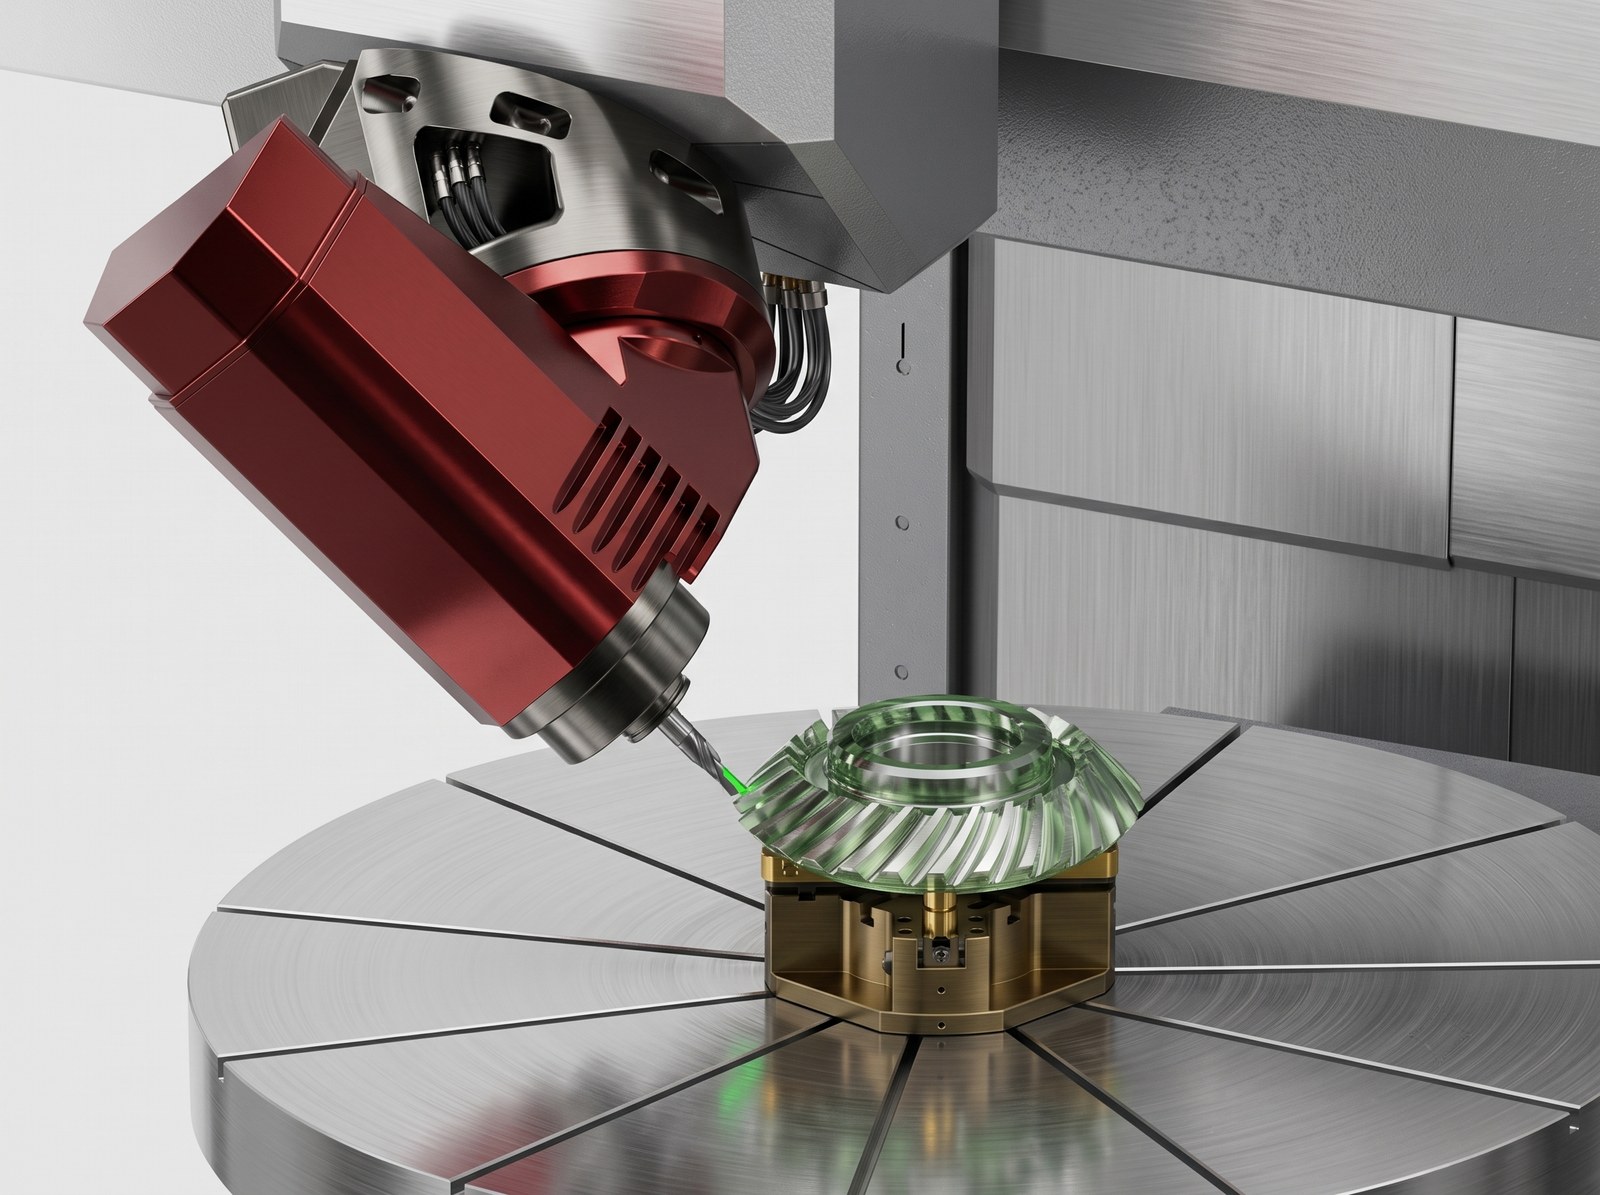
5-axis machining centre with swivel head and rotary table
3-, 4- and 5-axis milling

Exactly as the machine
will move it

Impellers, blisks and turbine blades leave no room for a second attempt. The trunnion, the swivel head and the pivot offsets are built exactly as they are on the machine, so the posture on screen is the posture of the machine.
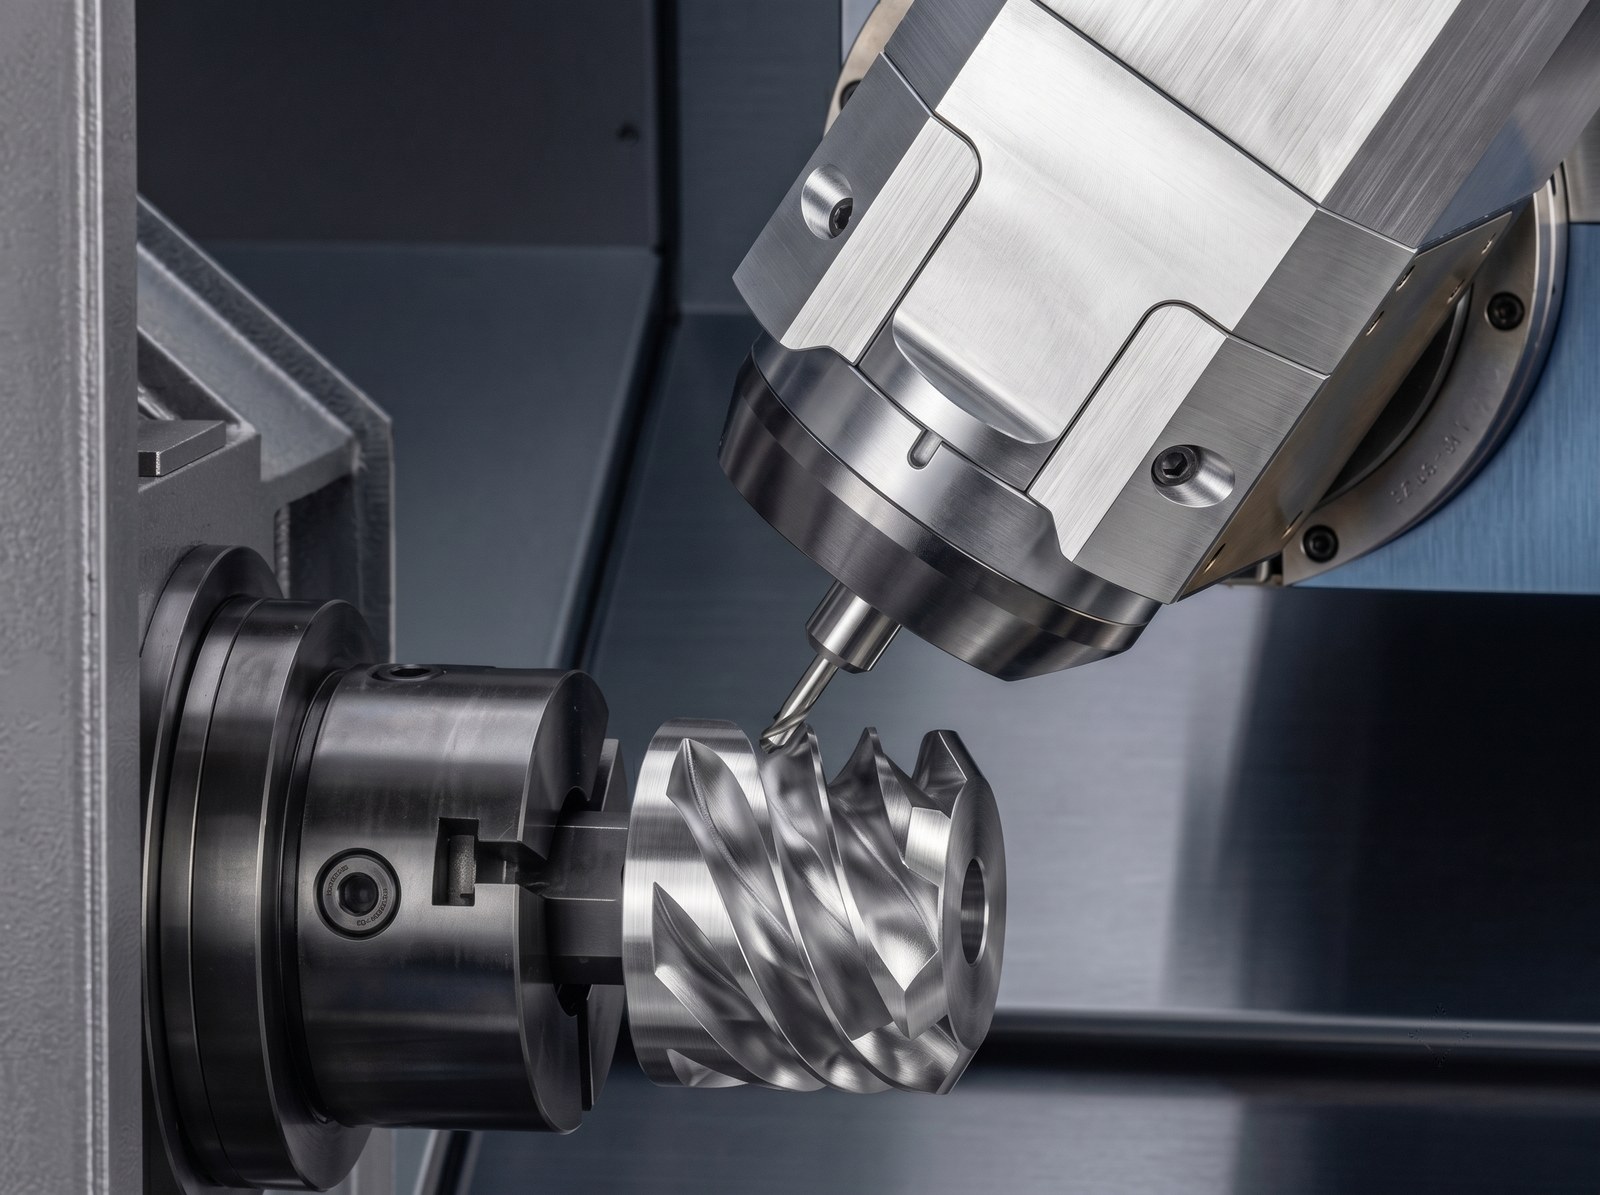
  • TCP (G43.4 / G43.5) and 5-axis tilted work planes (G68.2, 3+2 inclined faces)
  • Canned drilling and tapping cycles
  • Fanuc, Siemens, Heidenhain, Okuma, Mazak, Haas, Mitsubishi
B-axis mill-turn cutting a rotor held in the chuck
B-axis mill-turn

Turning and milling
on one spindle

One setup, and the B axis takes any angle while the job runs. Through index moves, offsets and work-shift changes, the part coordinate system is held exactly, right through to the sub-spindle.
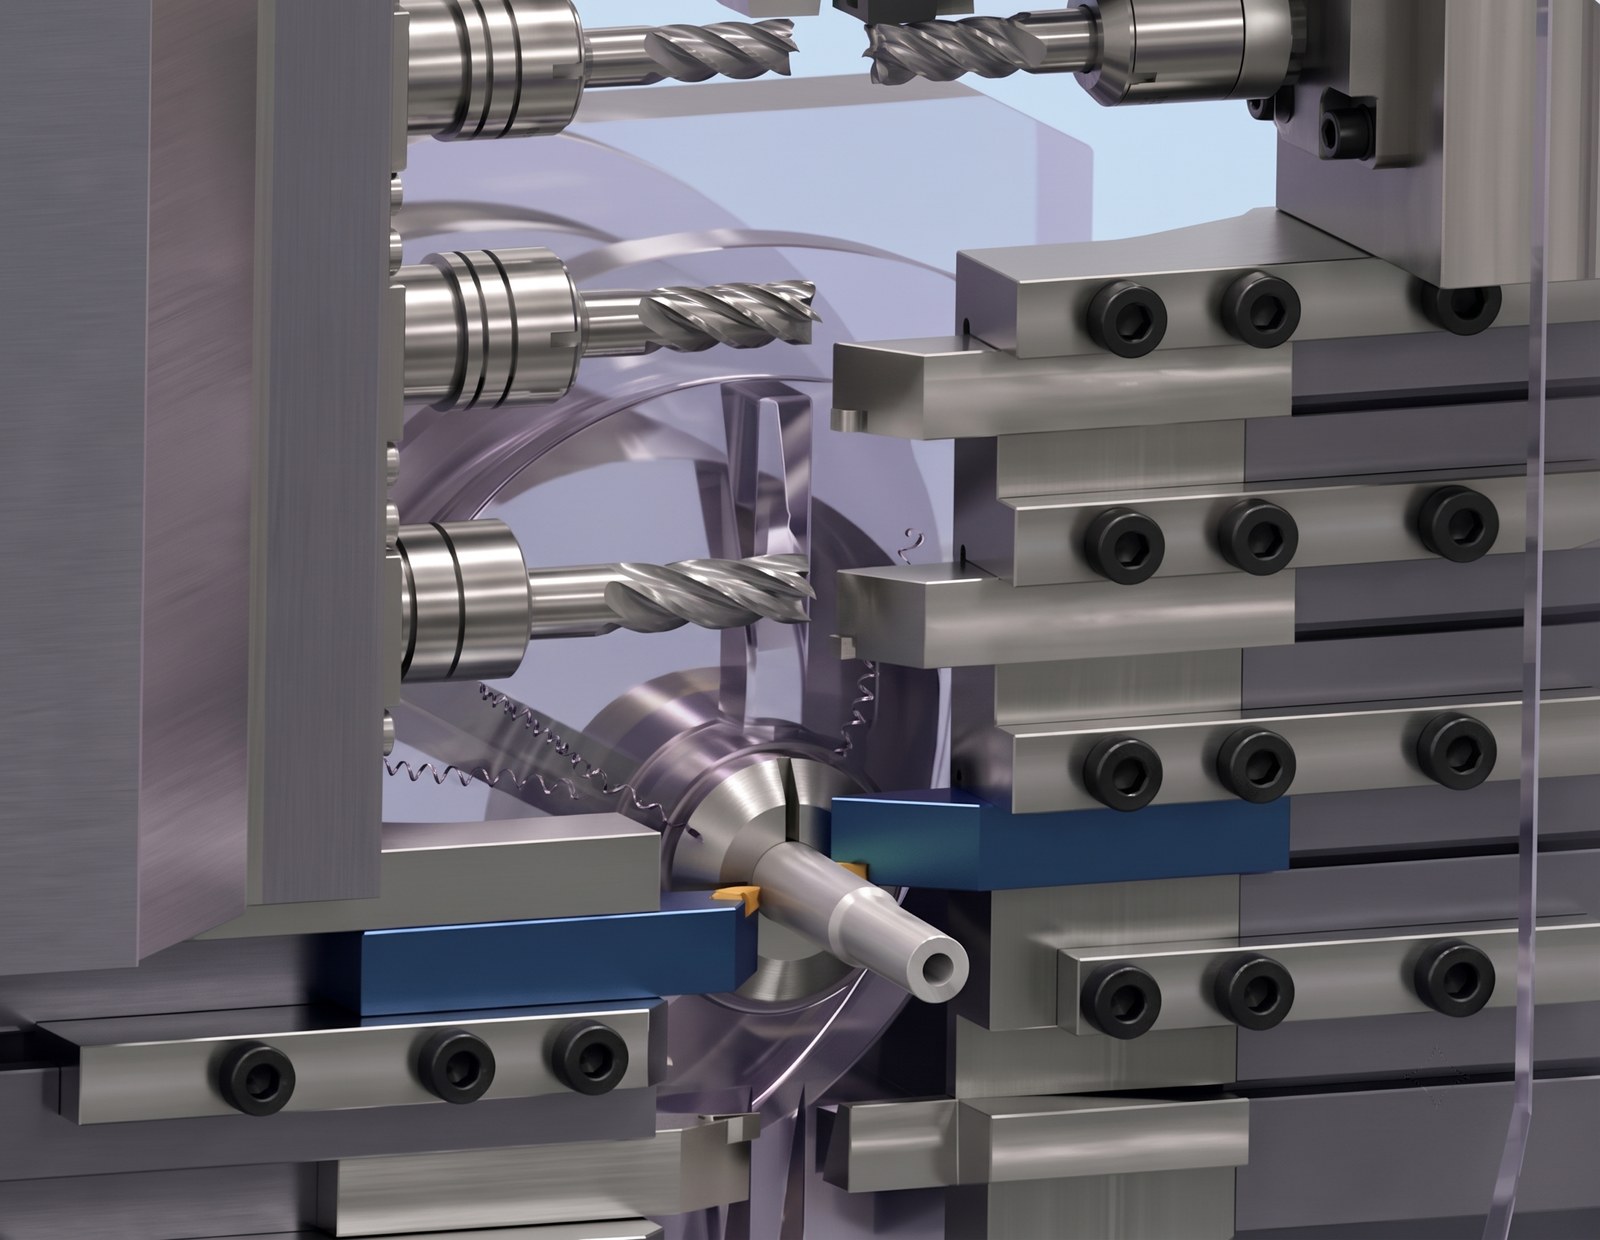
  • B-axis tool spindle turning, inclined-face milling and drilling, simultaneous 5-axis
  • Cylindrical (G07.1), polar (G12.1), G68.1 and CYCLE800
  • SMX, Integrex, NTX and Multus posts in machine coordinates
Swiss-type lathe with guide bush, gang tools and slender bar
Swiss type · 2 channels

Two channels you can
finally see

The guide bush, gang tools and the sub-spindle hand-off are the hardest work to picture in your head, and that is exactly where crashes happen. AicncX runs both channels together, in sync.
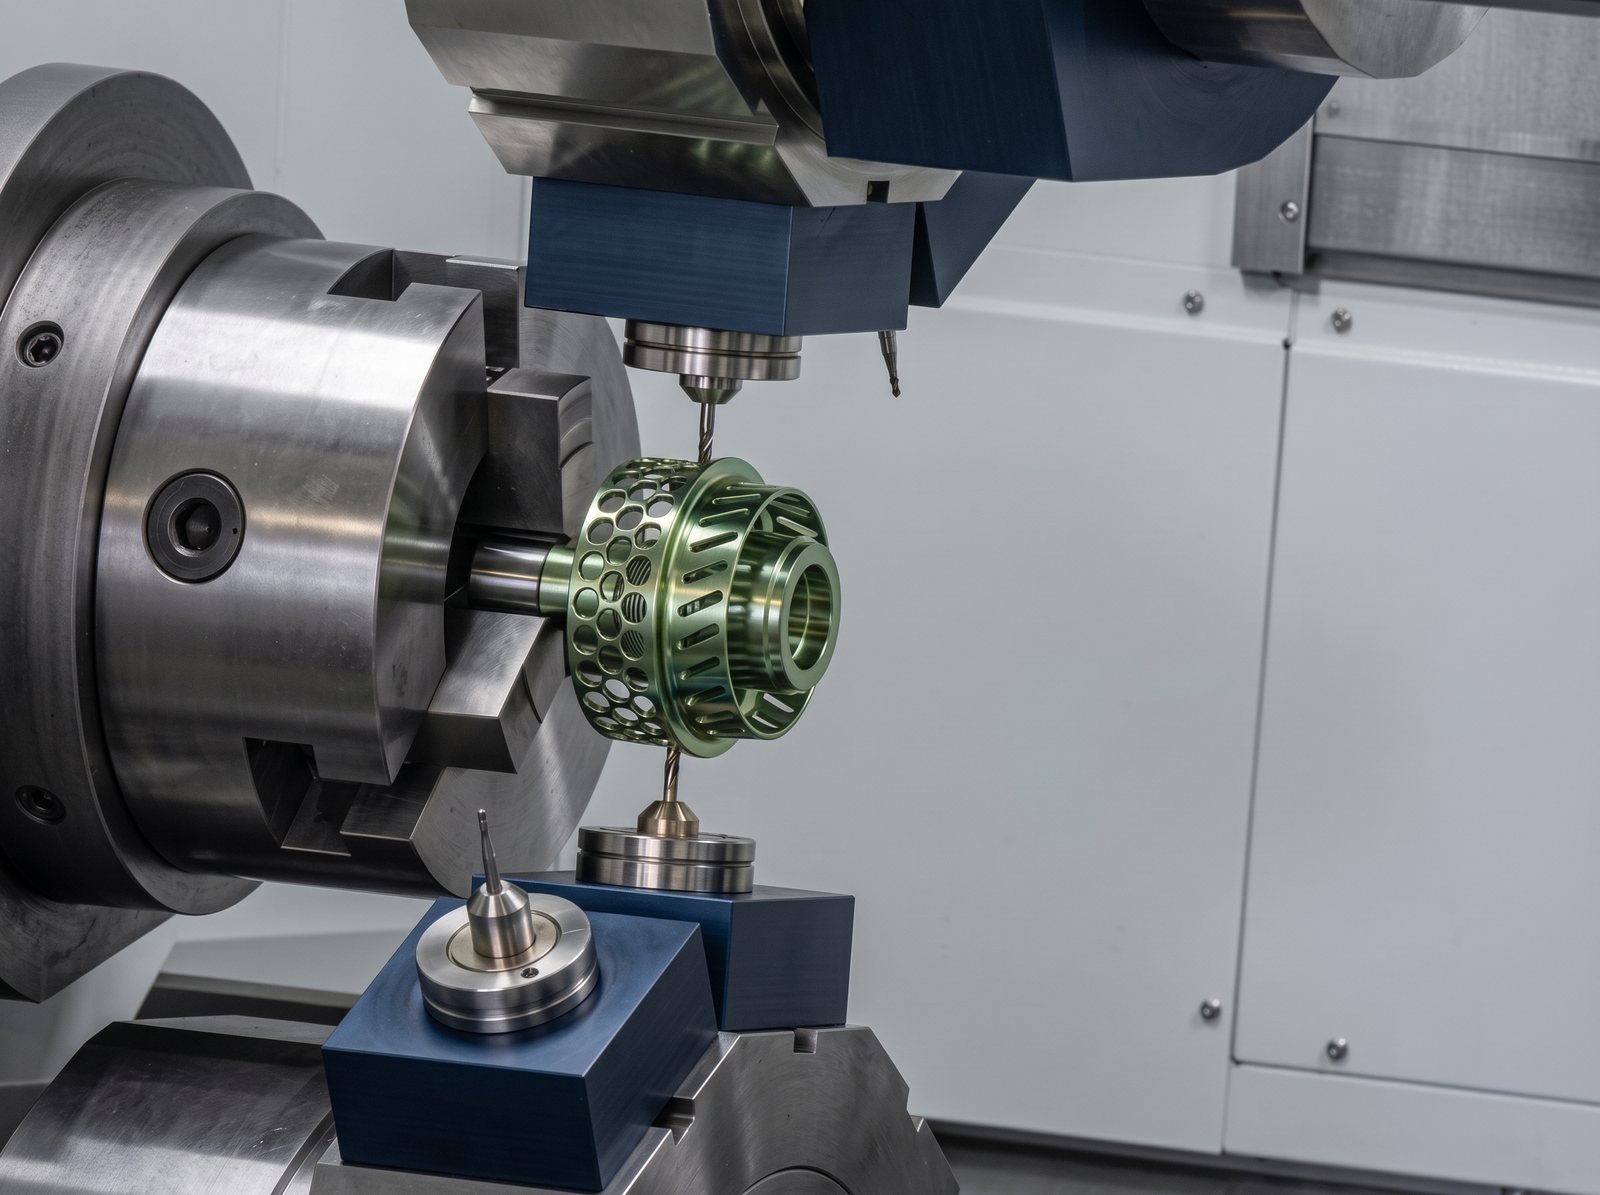
  • Channel 1 / 2 sync codes and waits on one timeline
  • Guide bush, back working, stock per spindle
  • Star, Citizen Cincom, Tsugami, Nomura, Hanwha
Twin-turret turn-mill cutting one part from above and below
Turn-mill · 2 turrets

Upper and lower turret,
cutting together

Two turrets machining one part at the same time carries a high crash risk and makes the program much harder to write. Per-channel stock, independent tool tables and sync waits all sit on one timeline.
  • Per-channel stock and independent tool tables
  • Sync waits between channels on the timeline
  • Lower-turret coordinate conventions per post
Wire EDM cutting a profile with upper and lower guides on a taper path
Wire EDM

Upper and lower guides,
cutting on a taper

Wire EDM is hard to check: the upper and lower faces follow different taper paths, with per-pass offsets and technology settings on top. AicncX reads it as the control does and shows both-face paths, offsets and the thread/cut points together.
  • Upper/lower taper two-face paths and per-pass offset
  • Technology files apply per-pass offset and conditions
  • Thread and cut points with punch/die direction
Also covered

The everyday machines, too

3-axis millingPockets, drilling, canned cycles, cutter comp.
4-axis & 3+2Indexed planes, rotary wrap, angle heads.
CNC latheRoughing cycles, threading, nose-R comp.
Sub-spindle lathePickup, back working, two stocks.